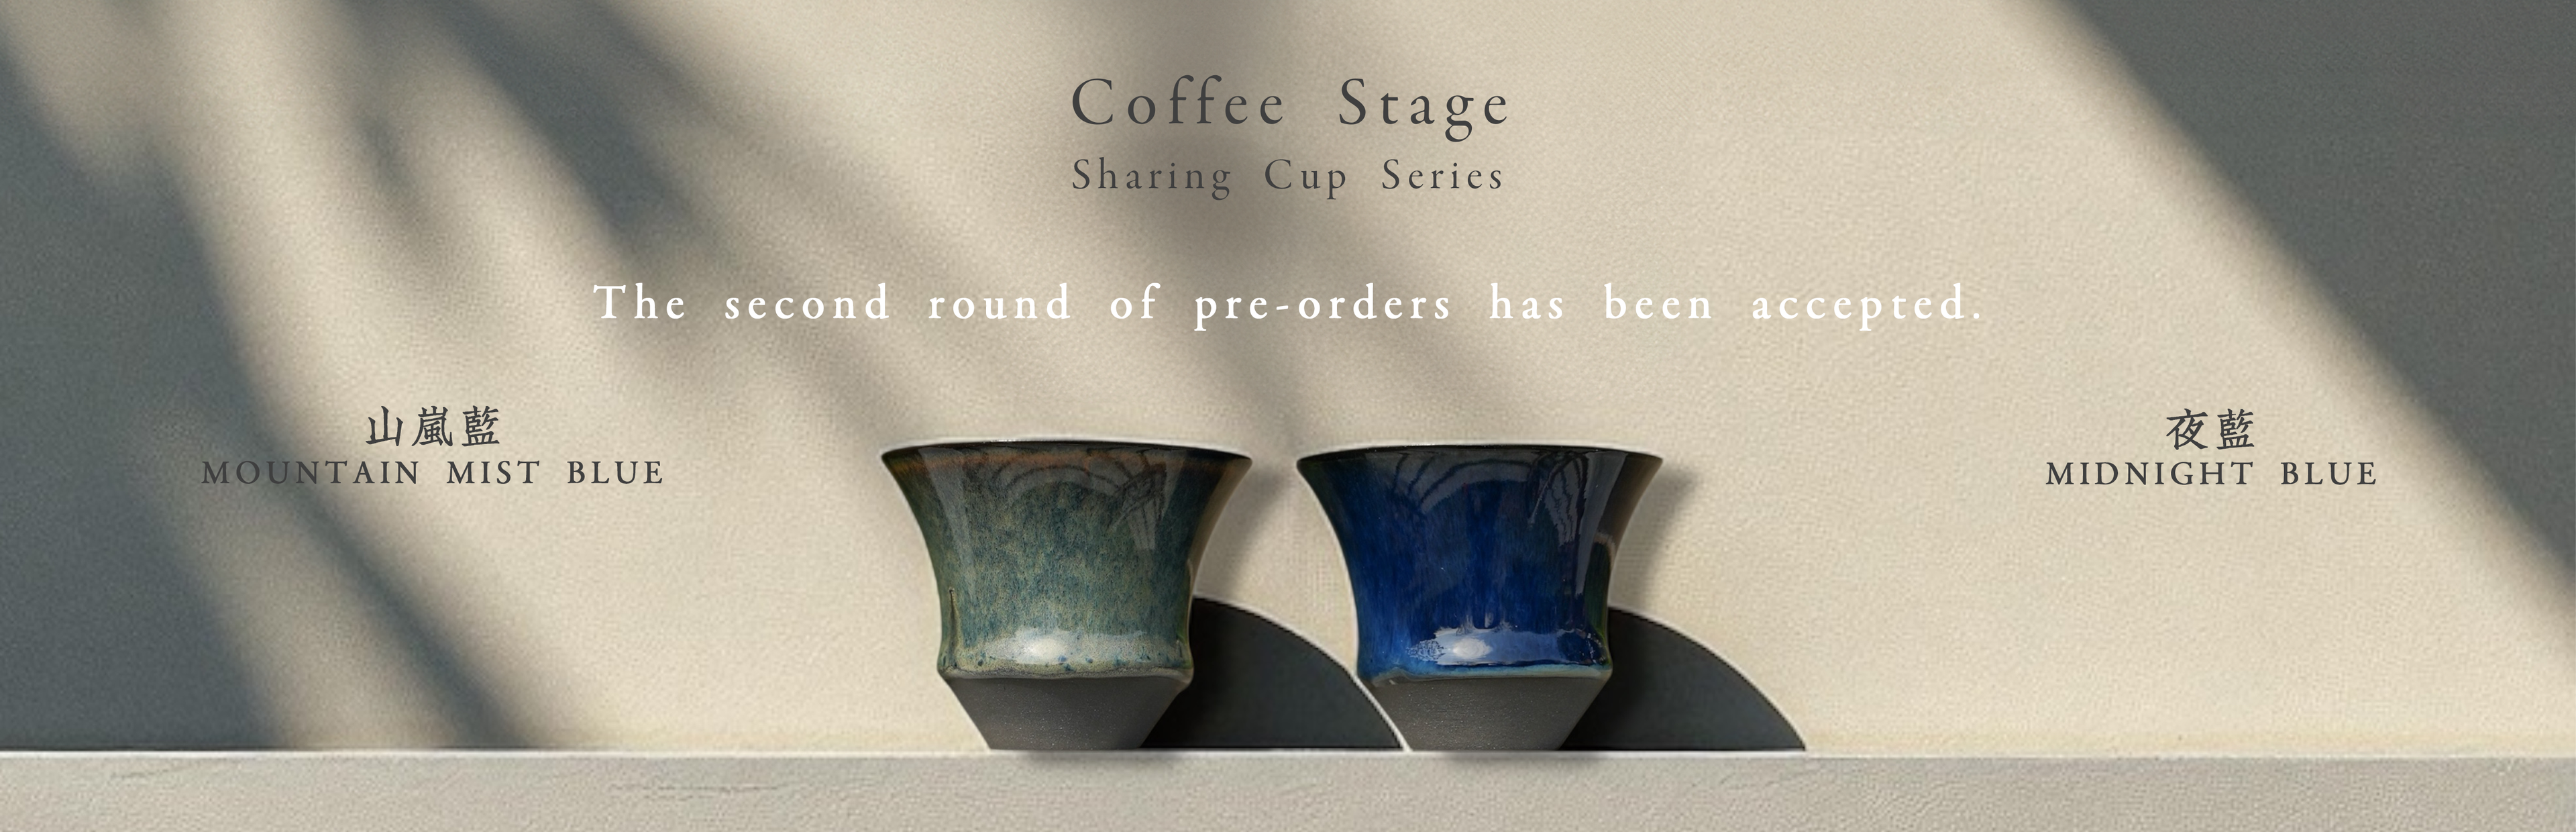

While we were making Sharing Cup, a friend asked: why not simply throw it on a wheel?
It is a reasonable question. When people think of handmade ceramics, many first picture hands drawing clay upwards on a spinning wheel as a cup slowly takes shape. For Sharing Cup, we chose slip casting, followed by trimming, drying and firing.
The reason goes back to where this series began. We wanted a contour suited to tasting in small sips: a body that curves inward, then opens out towards the rim. Once we found a direction we liked, we also wanted the curves and thicknesses within a batch to stay as consistent as possible. A mould gives us a starting shape we can return to.
But the same mould does not automatically produce the same finished cup. Much of the demanding work continues after forming.
Before the curve flares out, consider how the cup leaves the mould
A flowing profile looks like a single curve: inward, then outward. In production, it raises a very practical question: in which direction can the formed cup leave the mould?
If one part is wider than the opening it must pass through, it cannot simply be pulled out in one direction. The curve and the way the piece is removed must be considered together. We cannot settle every proportion first and treat the mould as an outer shell added at the end.

Left to right: S Size, M Size, L Size, Alpha Size, Beta Size.
This is also why physical pieces were still needed after digital exploration. A shape on screen can stay in an ideal state; an unfired cup has to face removal, support and further trimming. A suitable shape is only the beginning. It also needs a way to be made.
That does not mean we think wheel throwing is a poor method. Our priority in choosing this process was to give the selected contour a more consistent starting point during repeated production. If variation between individual pieces is the aim, the choice may be different.
Why does pouring in slip eventually leave a hollow cup?
The key to conventional plaster-mould slip casting is that the mould draws some water out of the slip. Clay close to the mould wall gradually forms a layer. When it reaches a suitable state, the excess slip that can still flow is poured out. What remains continues to firm up, and a little shrinkage makes it easier to remove. Read Digitalfire’s explanation of slip casting
This explains why casting time relates to wall thickness. But there is no number of minutes that works everywhere. The condition of the material, the mould’s water absorption and the rate at which the layer builds all need to work together. In everyday production, we still need to look at the unfired cup, rather than just a timer.

Reducing the rim’s sense of bulk is not simply a matter of shortening that time further and further. A thin wall still has to withstand removal and trimming. With a little less material formed, more attention is needed later to whether it is firm enough and can hold its shape while being handled.
This trade-off turns “thin” from a product description into a question we face every time we make a cup.
Other makers’ work also shows shape and process developing together
Digitalfire documents thin-walled open bowls and shows practical uses of 3D-printed parts to help align moulds and form pouring openings. View the original maker’s record
These examples do not give Sharing Cup a ready-made recipe, but they show how tools can also be used in the details of making. What we take from them is that shape and process can be considered together: when changing one part, look back at how it affects the next step.
Our difficulty also went beyond “drawing the proportions correctly”. Once the curve enters clay, there is more to consider. The distance between one sample cup and a batch that can be made repeatedly begins to grow.
Why can cracks appear after a cup leaves the mould looking sound?
Clay shrinks as it dries. If thin areas dry and stiffen first while thicker areas retain more moisture, the parts may not shrink together. As the clay becomes firmer, areas that could previously deform may no longer withstand that pull.
Digitalfire’s drying-disc test deliberately makes the centre and the edges dry at different rates to observe how cracks form. Some cracks appear later, even though the moisture difference that causes the problem was established much earlier. Read about drying shrinkage and practical examples
Applied to cup making, this explains why a crack calls for more than recalling the last action performed. The thicknesses of the rim, body and base, their exposure to air and how they dried earlier may all be worth revisiting. This is a general principle of ceramics; the actual cause in each case still depends on the particular piece and the conditions at the time.

So casting does not remove the need for the maker’s judgment. When to remove a piece, how far to trim it and how to let it dry still affect whether it keeps the intended shape. Bisque firing and glaze firing follow. The process names are short, but the condition of the cup changes at every stage.
A mould helps narrow the differences at the starting point; variation in materials and handwork remains. Nor should handmade production be used to excuse cracks. Natural differences in glaze colour and texture are distinct from problems that affect use.
With all that work, why still choose a thin rim?
The starting point is quite simple. We want the rim to feel less present when coffee reaches the lips, and the body’s curve to work with the tasting movement for more continuous small sips. That intended use is why we put extra effort into forming and the work that follows.

A thin rim is not everyone’s first priority when choosing a cup, though. Some people need a handle, some care about how much coffee they can pour at once, and others want a cup they can put in the dishwasher. Enjoying the details of contact at the lips and being willing to care for a cup are both part of the practical choice.
The next time you pick up a cup, notice how it feels against your lips, then look at the lines inside and outside the body. For us, those lines connect two kinds of work: deciding what we want from drinking, and finding how to make it physical, then make the next one.
If you would like to choose a cup from here, compare the practical uses of the five Sharing Cup models according to your usual serving size and way of drinking. To first explore how a sip feels, return to cup curves and the first sip of coffee and try it once with the cups you already have.